Welcome to your Saved Items
View saved favorites,build-your-own custom bags or products.
For faster checkout sign in to your account.
Your Shopping Bag
Your shopping bag is empty.
Custom inquiry
Please enter your enquiry requirements
Demand
Name
E-mail
Contents
Inquire
Subscribe for more information

Choose XCGS

Choose Good Quality

Suzhou Star Group New Materials Group Co., Ltd. ("Star Group Group") was founded in 1999 and is an integrated solution provider in the field of ESD packaging and consumables. With 27 years of deep industry experience, the Group has become a national high-tech enterprise in domestic ESD protection, driven by core technologies, six manufacturing bases, global layout, and stringent quality control.

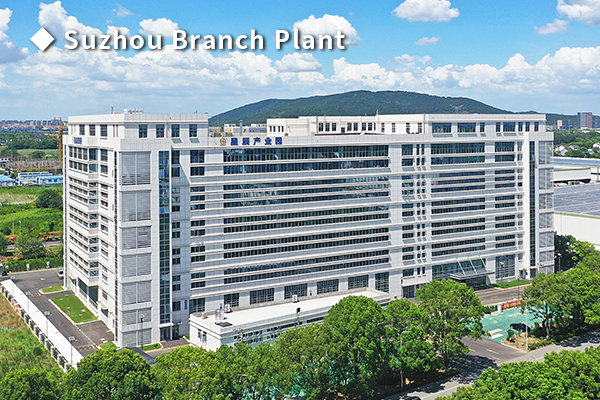
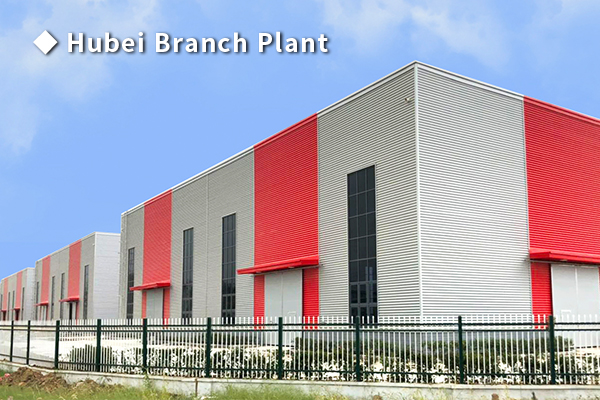
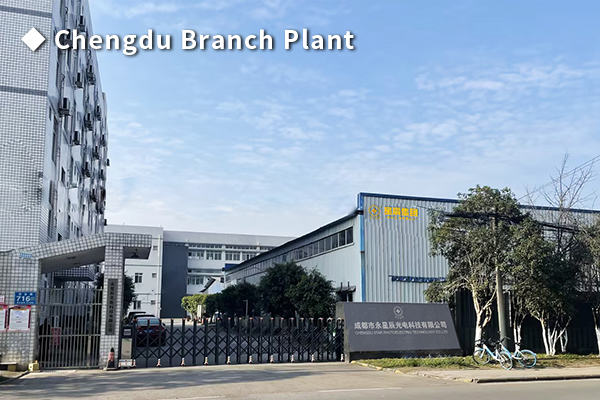
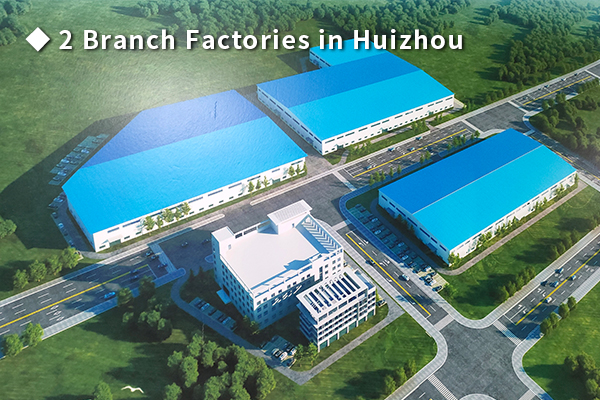
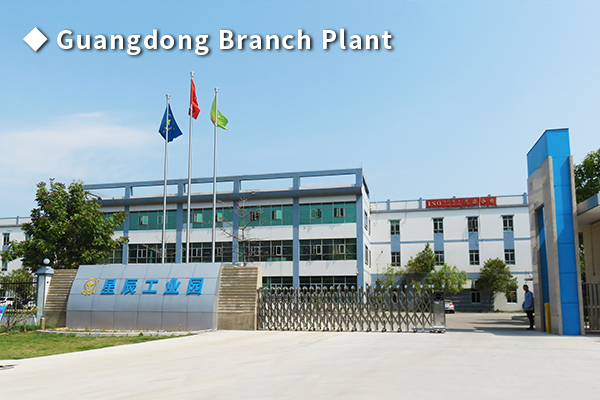
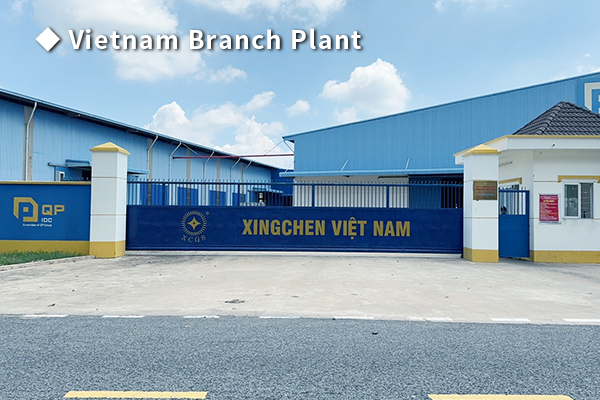
Headquartered in Suzhou, the Group operates eight factories across six manufacturing bases in Suzhou, Dongguan, Chengdu, Hubei, Huizhou, and Vietnam; and has overseas sales offices in the U.S. and Singapore. It has established an industrial layout of "Yangtze River Delta as the core, radiating to the Pearl River Delta, deeply cultivating the central and western regions, leading Southeast Asia, and covering the globe." Its business covers over 100 countries, and it can export to any designated port worldwide per customer requirements, meeting diverse product needs with a steady global footprint.

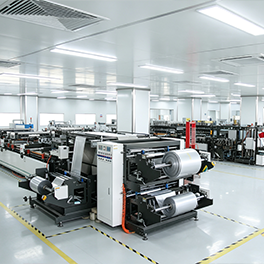
Star Group Group owns over 200,000 m² of modern production facilities, equipped with a 5,000 m² Class 1,000 cleanroom and a 1,000 m² Class 100 cleanroom, with product quality meeting the high international standards of the semiconductor industry. The Group holds over 100 proprietary patents. With core product strengths, it has established long-term strategic partnerships with more than 50 Fortune 500 companies worldwide.

Star Group Group fully supports the production of high-end products for global electronics manufacturing and cleanroom ESD protection. Its products are widely used in semiconductors (wafers, chips), electronic components, optics (LCD optoelectronics, LCD modules, optical modules, etc.), precision electronics, automotive electronics, medical devices, aerospace, and other fields, providing safe and reliable one-stop supporting products for precision manufacturing, electrostatic protection, and cleanliness control across various industries. It has long served industry leaders such as Samsung, STMicroelectronics, Renesas, and AMD, making it a safe and reliable core ESD protection supplier for the chip and semiconductor sectors.

Amid the global semiconductor supply chain wave, Star Group Group adheres to a long-term philosophy. With a steady pace of "integrity, pragmatism, stability, and innovation," it deepens its core products and builds a solid ESD protection foundation for every customer. With a century-long goal, Star Group Group is committed to contributing lasting and determined strength to industry progress and social value.

8 Factories
200000 m²
Production Base
8 Factories
Production Line
1000 +
Employees
100 +
Patents & Certifications
Workshop Display
Efficient and Safe XCGS Workshops

Star Group boasts a production area of 200,000 ㎡, including multiple Class 1000 and Class 100 cleanrooms with a total area of over 10,000 ㎡.

All workshops are equipped with central air conditioning, air purification systems, exhaust systems and other hardware facilities.

Film blowing workshop
Coating workshop
Printing workshop
Bag-making workshop
Certifications Display
Trustworthy XCGS Quality with Patents and Certifications

Star Group owns 89 independent patents, 2 international patents and 3 registered trademarks. Audited by SGS, we comply with ISO9001, ISO14001,

OHSAS18001 and work safety standards, holding RoHS, REACH and multiple patent certificates.

Patents and Certifications

Authoritative Certification

XCGS is trustworthy
REACH
Registration, Evaluation, Authorization and Restriction of Chemicals
TUV
Technische Überwachungs Vereine
RoHS
Restriction of Hazardous Substances
SGS
SGS International Certification
AWTA
Australian Testing Agency Certification
Best-selling Packagings of XCGS
One-to-one High-end Customization

According to the customer's needs, we design the packaging structure and pattern.

To satisfy the vast range of demands of our clients, we have a global sales network with quick response times and short delivery windows.

About XCGS
Bringing Quality Packaging to Life
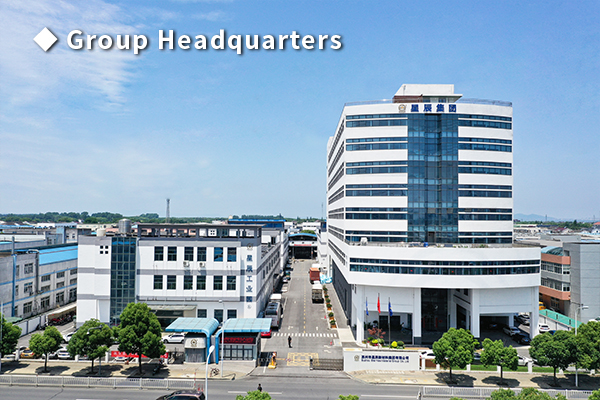
XCGS's headquarter office building covering an area of 40 acres, with a building area of 200,000 square meters

(including 25,000 square meters modern scientific research buildin).

With more than 1000 employees, it has an independent R&D and testing center, equipped with 20+ sets of testing equipment.

The internal facilities are perfect, creating a multi-functional space integrating work and leisure.

Recreation area
Office area
Showroom area
Fitness area
Subscribe for more:
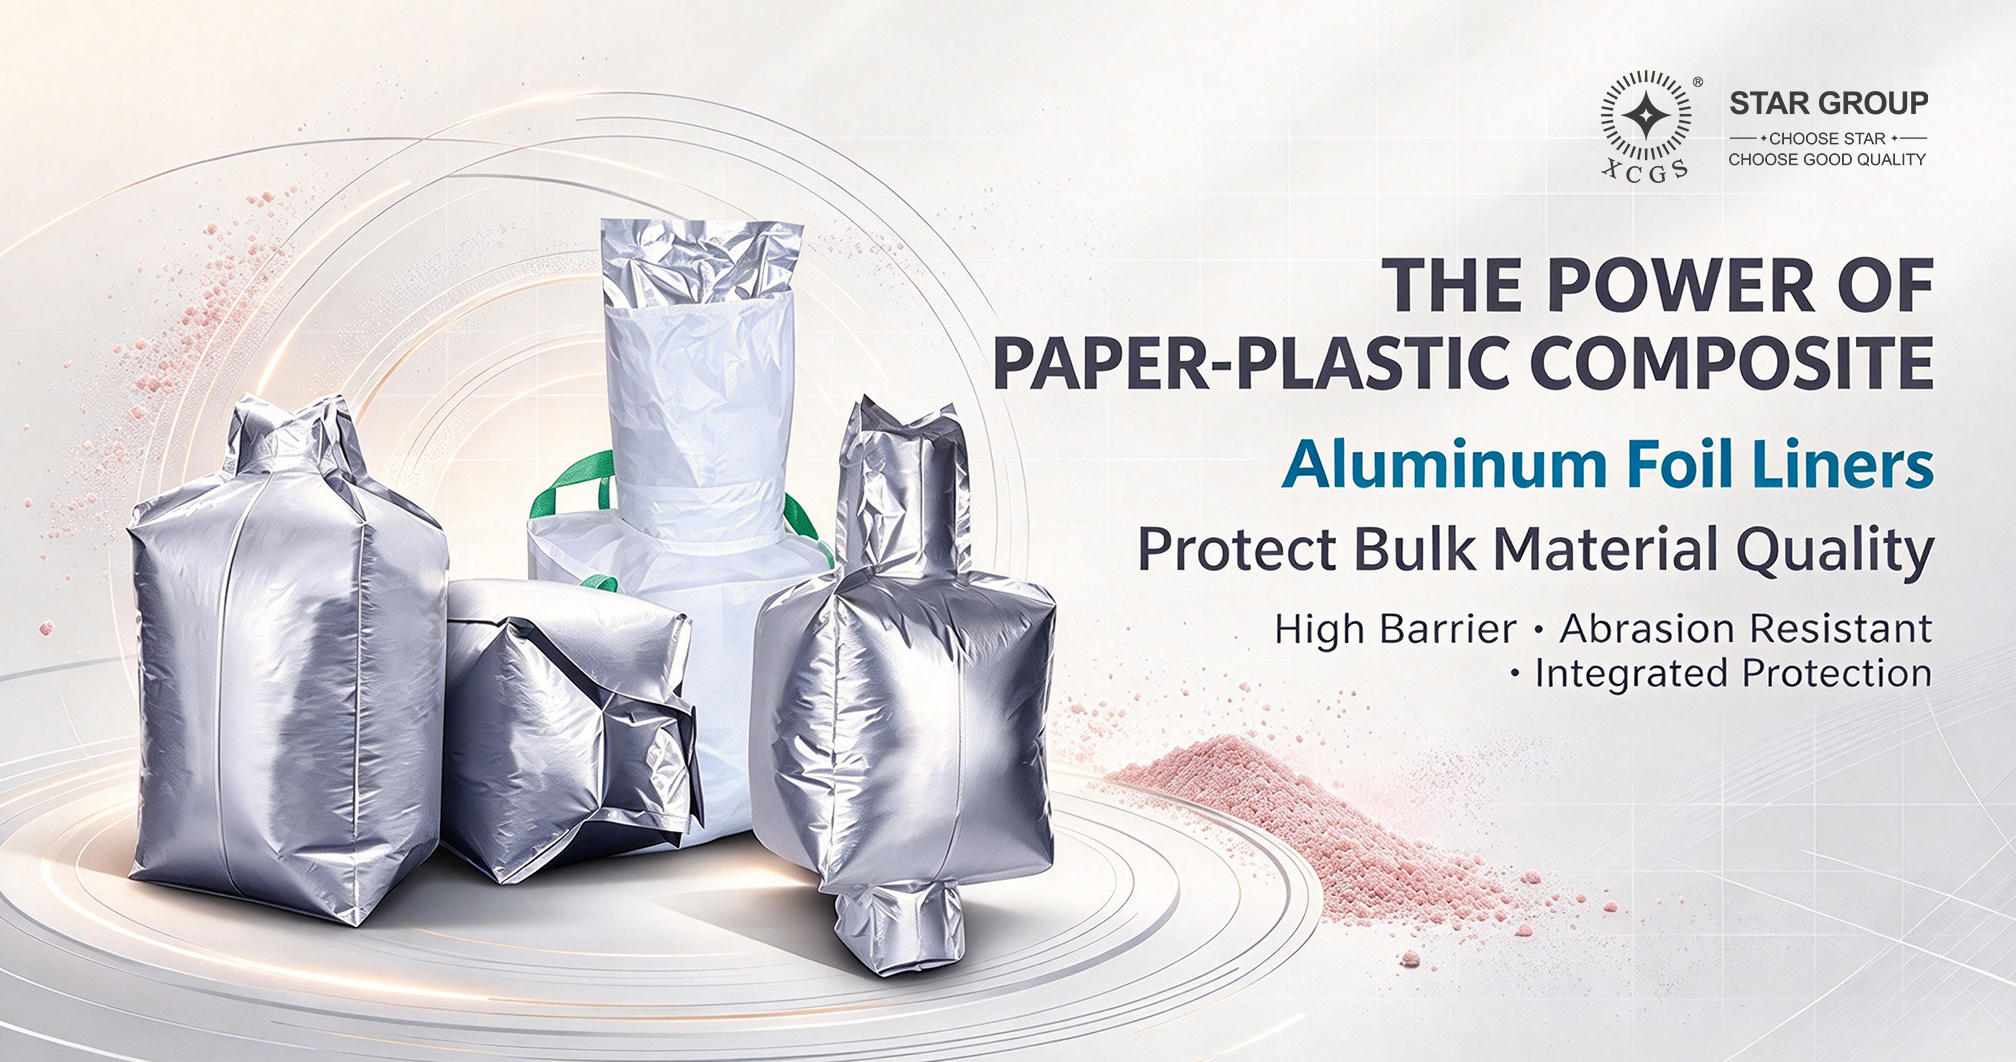
In the transportation of bulk materials, the outer bag bears the load, yet it is the seemingly inconspicuous inner component — the flexible FIBC liner — that often determines material quality. For highly environment-sensitive materials such as lithium battery powder, plastic pellets and chemical raw materials, the barrier performance of the liner directly decides whether the materials suffer from moisture ingress, oxidation or deterioration. Xingchen Group’s aluminum foil liners adopt high-barrier aluminum foil lamination technology to safeguard the quality baseline of bulk materials.
Tjj
October Thu , 2026
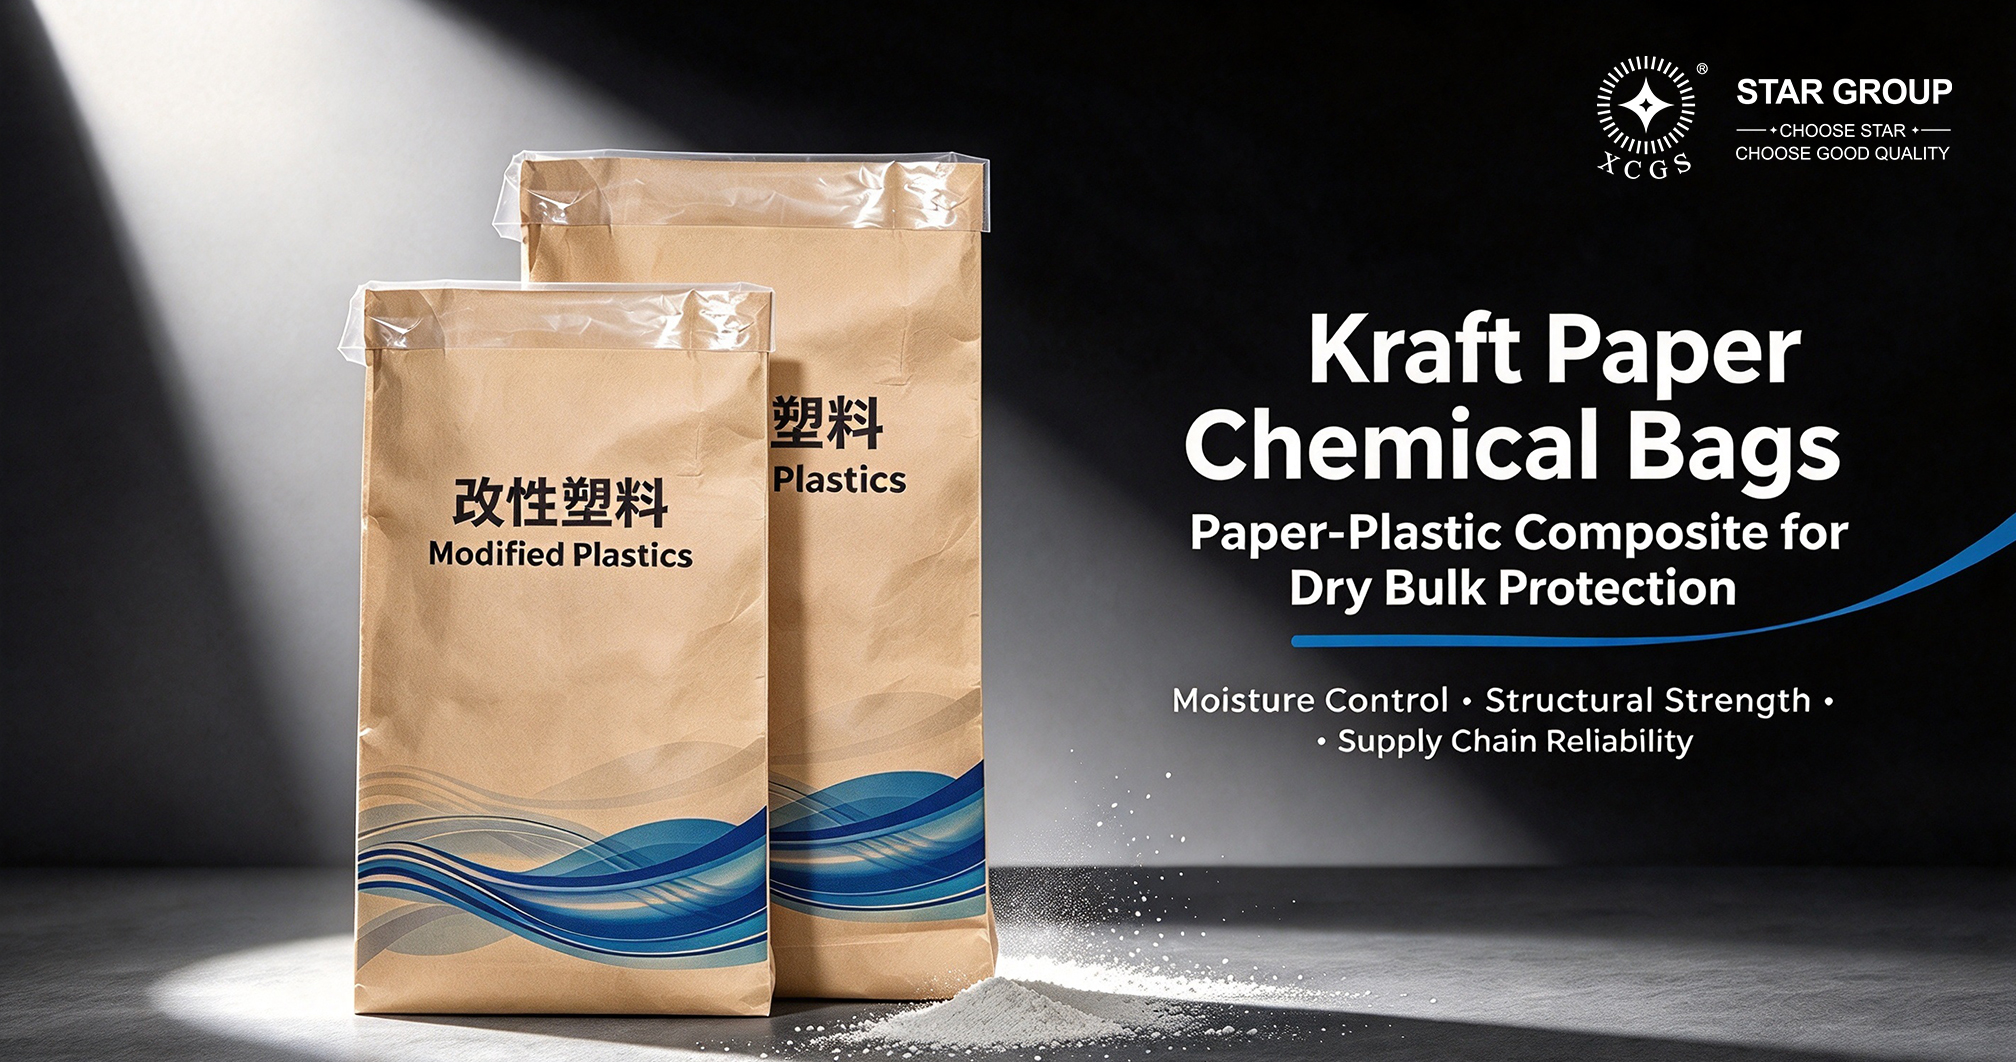
Packaging for chemical raw materials has always been one of the most critical links in the industry. Powder and granular chemical materials are highly susceptible to moisture and oxidation. Insufficient packaging protection will severely degrade raw material quality and impair the performance of downstream finished products. As a typical application of paper-plastic lamination technology, kraft chemical bags serve as an important packaging option for bulk materials in the chemical industry, featuring sound structural strength and excellent moisture resistance. Drawing on over two decades of industrial packaging expertise, Xingchen Group delivers reliable kraft chemical bag solutions for chemical raw materials.
Tjj
October Thu , 2026
Among packaging solutions for bulk materials, paper-plastic heavy-duty bags stand as a classic option combining mechanical strength and protective performance. By laminating plastic and paper materials, they fulfill load-bearing and barrier requirements that can hardly be achieved by a single material alone. With over two decades of dedication to industrial packaging, Xingchen Group supplies dependable kraft heavy-duty bags for bulk materials in chemical, construction, agricultural and other industries, supported by mature paper-plastic lamination technology and strict quality control.
Tjj
October Wed , 2026
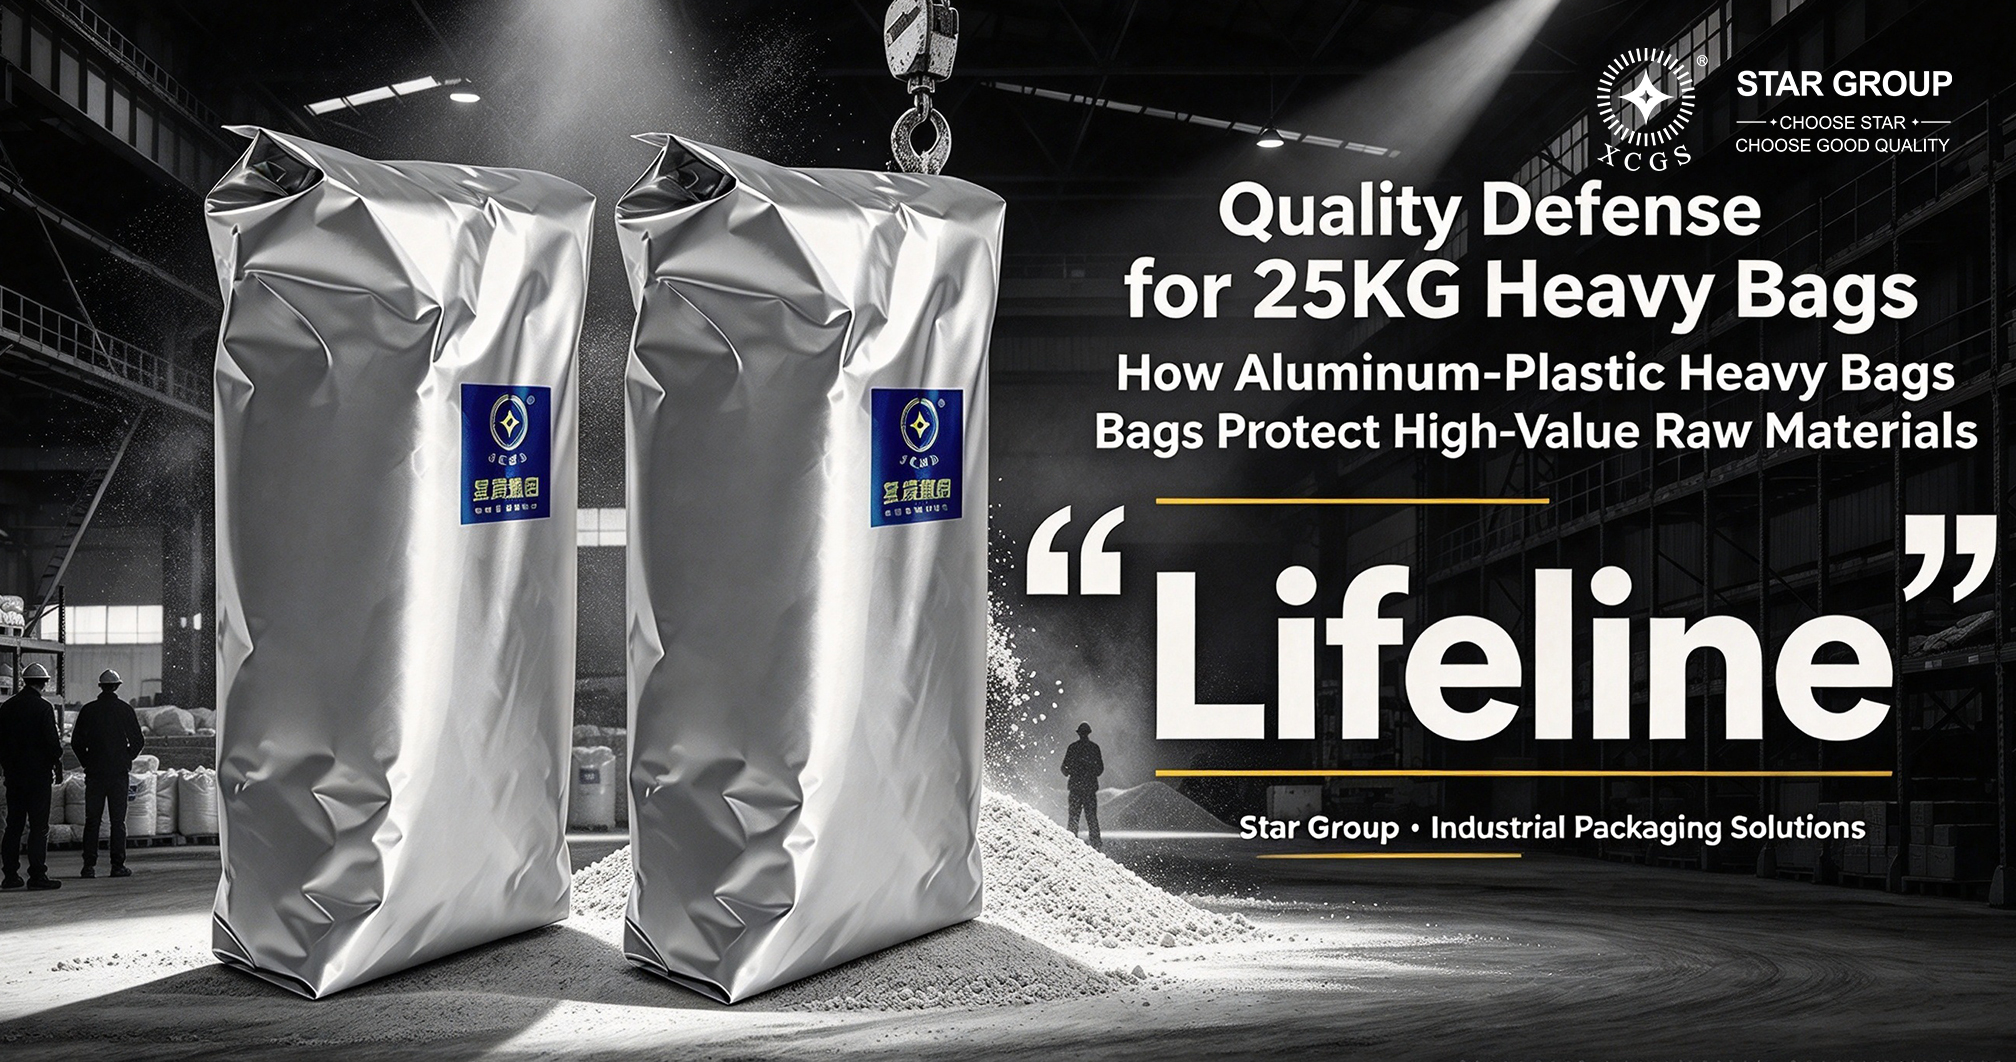
In industries such as chemical engineering, pharmaceuticals, electronics and food, damage to the packaging of a single 25kg raw material bag may lead to losses worth thousands of yuan, alongside a string of knock-on consequences including shipping disputes and erosion of customer trust. Statistics show that up to 30% of customer complaints stem from packaging leakage, moisture ingress or insufficient load-bearing capacity. As a direct manufacturer with over two decades of experience in industrial packaging, Xingchen Group builds a solid quality barrier for high-value raw materials with products including aluminum-plastic heavy-duty bags.
Tjj
October Wed , 2026
Among packaging solutions for bulk solids, aluminum-plastic FIBCs have emerged as a key option for chemical, construction, agricultural and other industries, thanks to their unique combination of structural strength and barrier performance. They integrate the outstanding barrier properties of aluminum foil with the toughness of plastic materials, delivering an all-in-one protection solution for high-value and highly sensitive bulk materials. With over two decades of dedication to industrial packaging, Xingchen Group supplies trustworthy aluminum-plastic FIBC products via aluminum-plastic lamination technology and a rigorous quality control system.
Tjj
October Tue , 2026
In the field of industrial packaging, certain materials require packaging capable of supporting ton-level loads while resisting the invasion of moisture vapor and oxygen. These include high-value bulk materials such as lithium battery powder, chemical raw materials and plastic pellets. Conventional packaging often fails to satisfy this dual requirement of heavy load endurance and superior barrier performance. Xingchen Group’s aluminum foil FIBC adopts multi-layer composite structures and strict in-house production controls, delivering a solution combining mechanical strength and barrier protection for such materials.
Tjj
October Tue , 2026
In modern industrial logistics, transporting large-volume bulk solids is far more than simply filling bags and loading them onto trucks. For powder and granular raw materials, moisture ingress, oxidation and contamination during transit may degrade the quality of entire shipments and incur substantial losses. How to maintain material quality while enabling high-capacity, high-efficiency transportation? Xingchen Group’s flexible FIBC liner delivers the solution. Paired with outer bulk bags, these high-barrier liners form a moisture-proof and oxygen-resistant inner shell to safeguard sensitive materials.
Tjj
October Mon , 2026
With the rapid growth of new energy vehicles, energy storage systems, photovoltaic equipment and other industries, the transportation and warehousing demands for new energy and chemical raw materials such as lithium battery cathode powder, lithium iron phosphate, solid-state battery additives and engineering plastic pellets keep rising. These high-value materials impose stringent requirements on packaging: it must withstand heavy loads of several tons and hoisting operations, while isolating moisture and oxygen in the air to prevent powder from dampening and oxidative deterioration. Drawing on over two decades of experience in industrial packaging, Xingchen Group delivers a complete solution balancing strength and barrier performance for new energy raw materials, adopting composite heavy-duty packaging consisting of a woven outer bag and an aluminum foil inner bag.
Tjj
October Mon , 2026
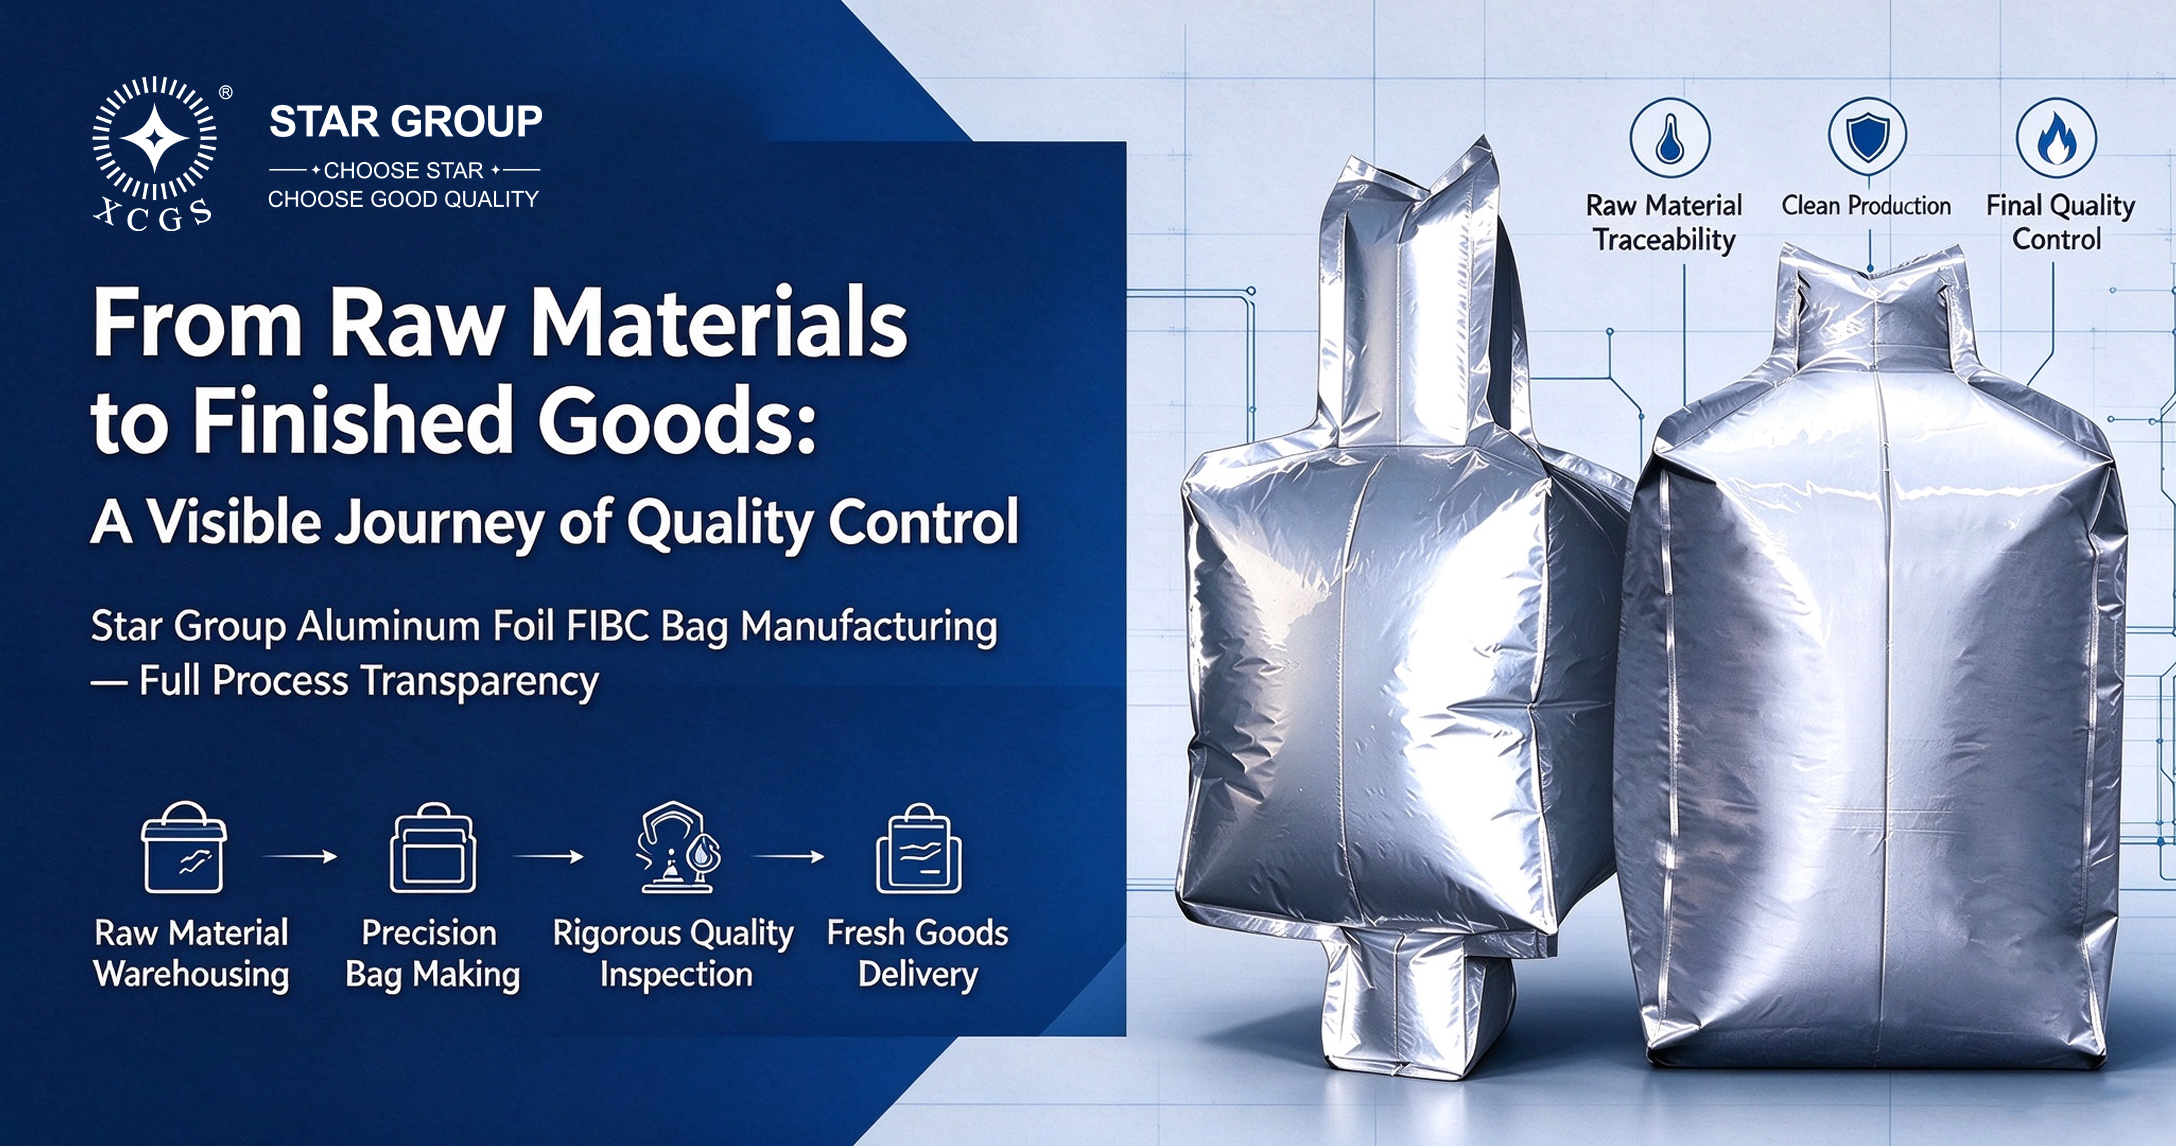
Inside the clean production workshops, automated equipment carries out precision lamination and bag making. Rigorous standards are applied throughout quality inspection — not every bag can pass final inspection. Additional production steps are implemented to guarantee that every delivered aluminum foil FIBC bag is a trustworthy product for customers. The finished goods warehouse follows a make-to-order delivery model without overstocking, ensuring every supplied bag is freshly produced.
Tjj
October Fri , 2026
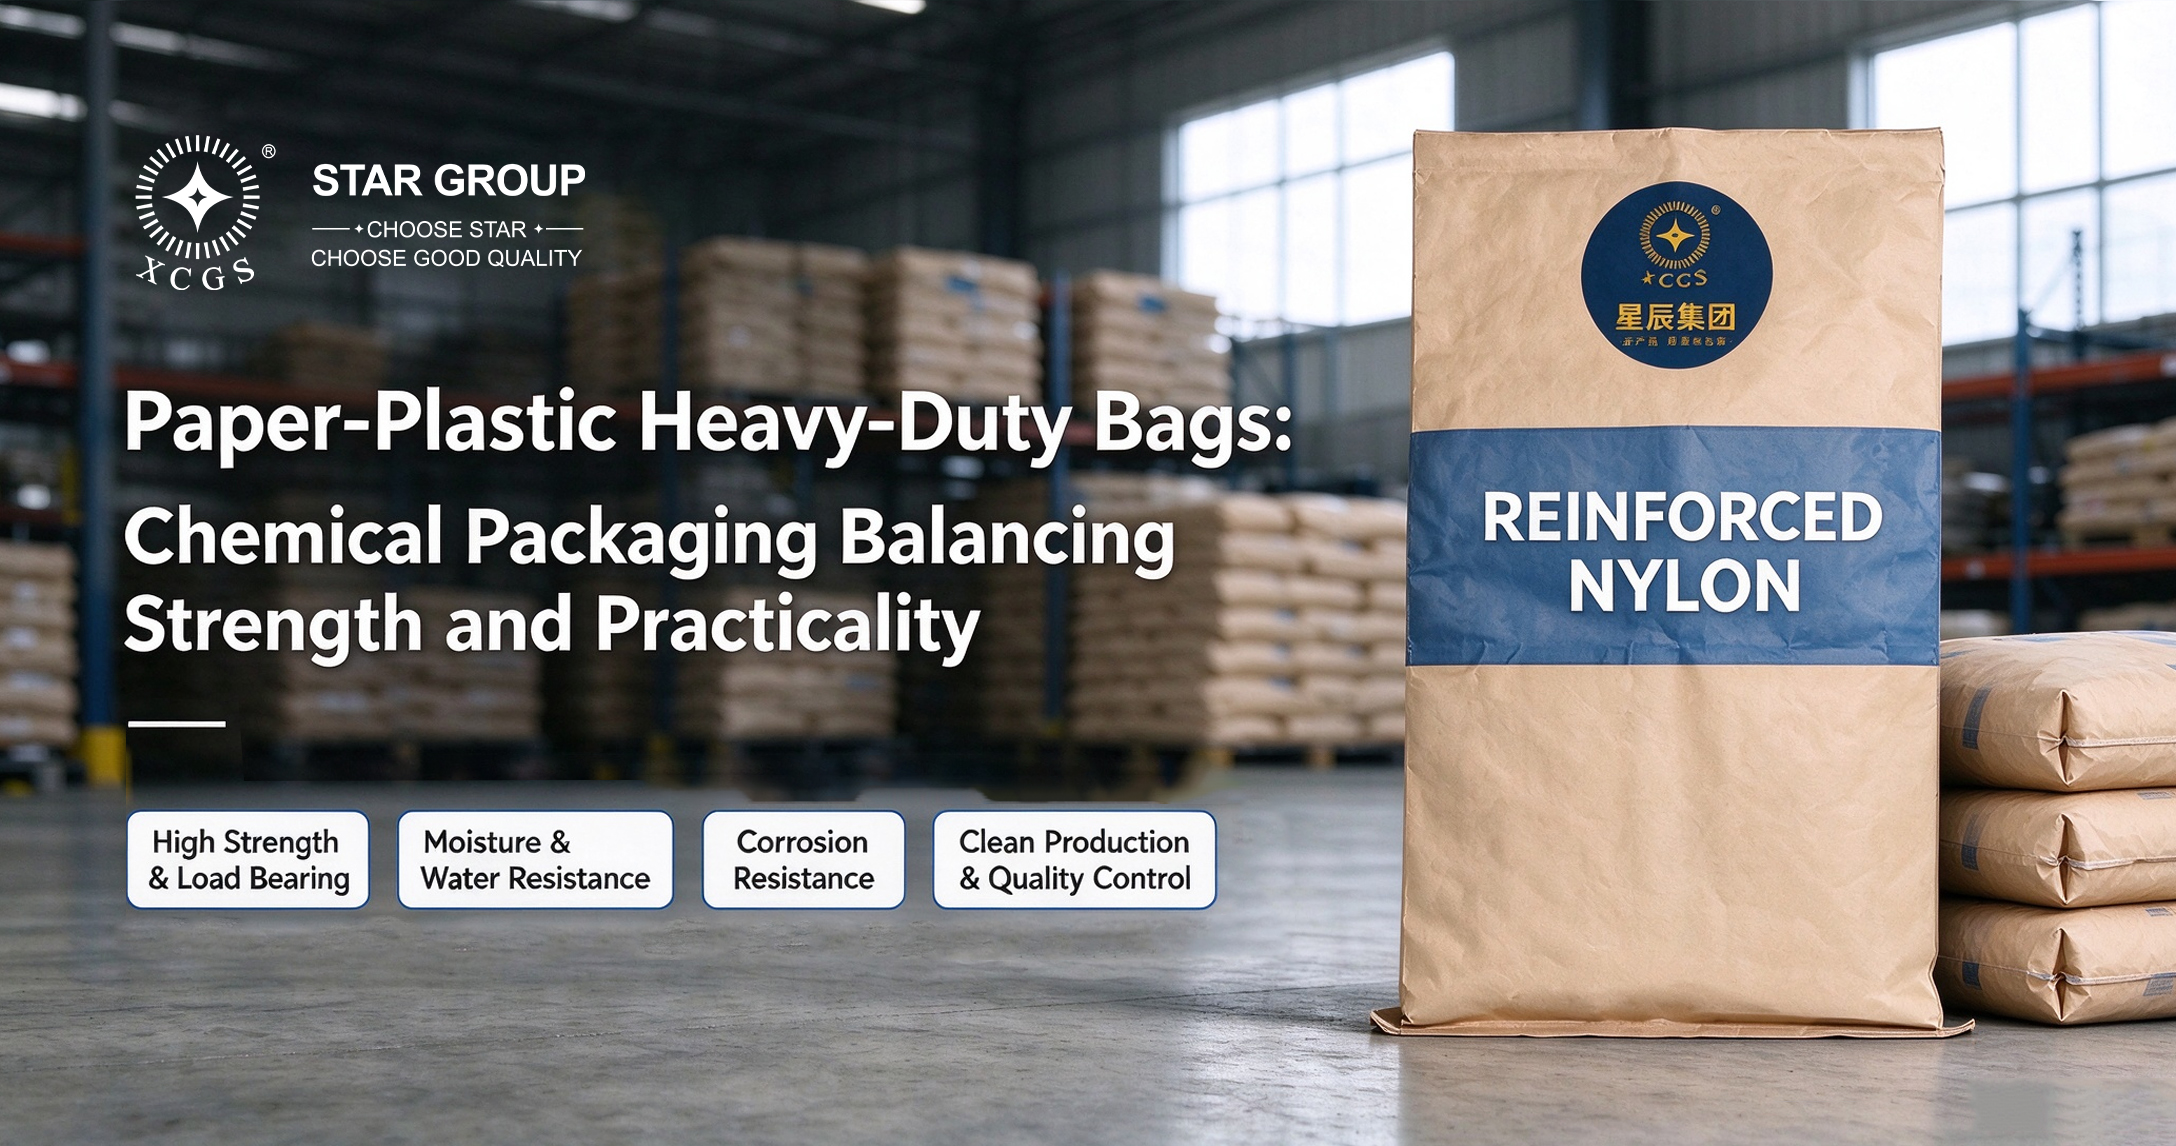
Paper-plastic heavy-duty bags are heavy-duty packaging bags laminated from plastic and paper materials. Featuring high tensile strength, moisture resistance, water resistance and corrosion resistance, they are widely adopted in chemical, construction, food and pharmaceutical industries. They combine the excellent printability of paper with the moisture barrier performance of plastic, facilitating brand information printing and offering reliable protection for packaged materials.
Tjj
October Thu , 2026
Powered By XCGS:
Copyright 2026 Suzhou Star New Material Group Co, ltd. All Rights Reserved 苏ICP备14029599号-1
Tel:+86 18915550561