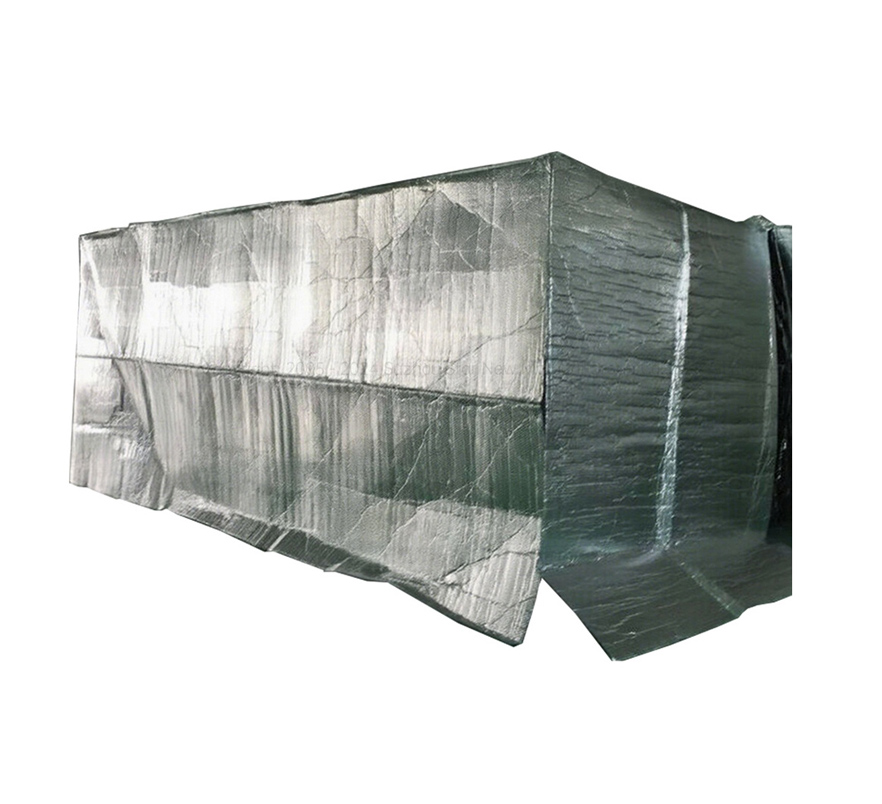
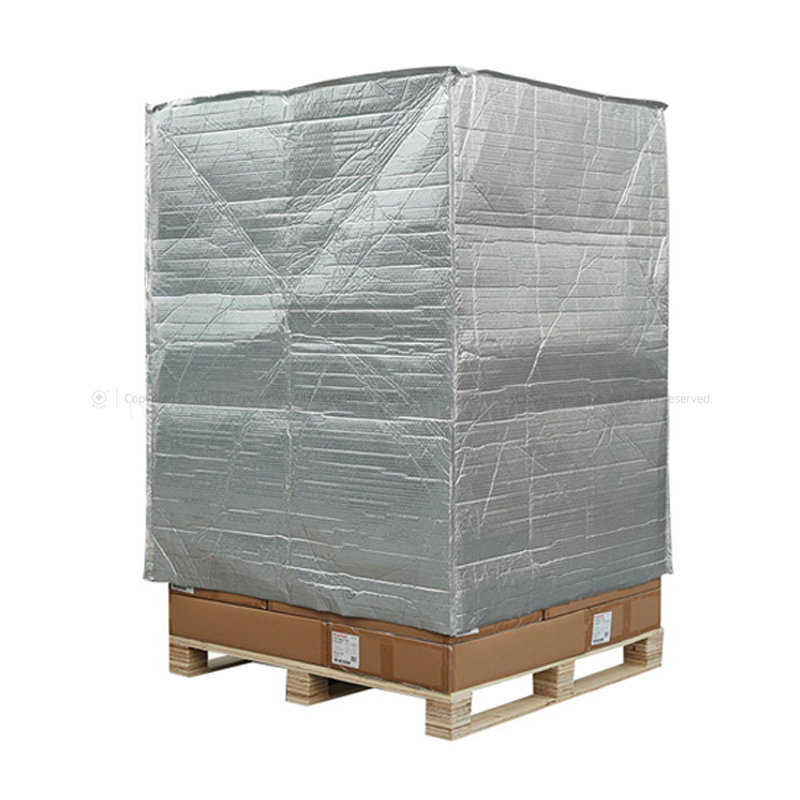
Industries including chemical, pharmaceutical, electronics and food impose stringent packaging requirements for certain high-value goods. Such packaging must deliver moisture and oxidation resistance alongside solid mechanical strength and tight sealing. Aluminum-plastic heavy-duty bags are premium packaging solutions engineered for these demands. Built on multi-layer composite structures, they integrate high barrier performance, high tensile strength and excellent sealing properties to serve as reliable protection for the storage and transportation of high-value products.
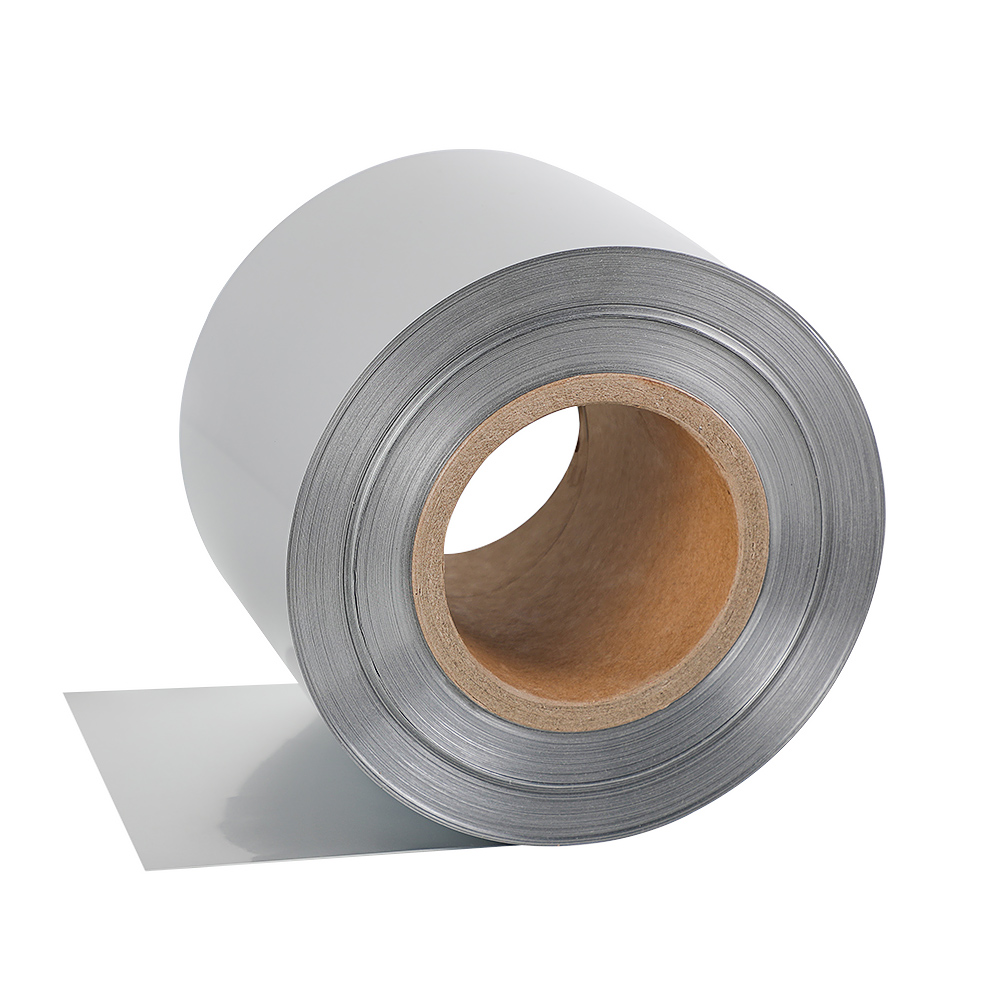
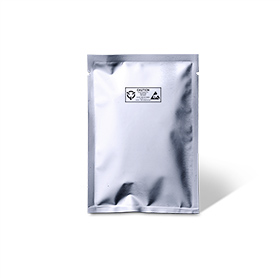
Aluminum-plastic heavy-duty bags are laminated with multi-layer materials (PET+AL+NY+PE), forming high-performance premium packaging materials. Their advantages are reflected in multiple dimensions: outer layers offer great strength and wear resistance, while inner layers feature outstanding heat-seal performance and sealing capacity. The aluminum foil layer effectively blocks air, water vapor and light to prevent oxidation, moisture ingress and deterioration of contents. With high strength and superior barrier properties, aluminum-plastic heavy-duty bags are widely adopted in pharmaceutical, chemical, electronics and food sectors, especially for high-value products with rigorous packaging requirements.
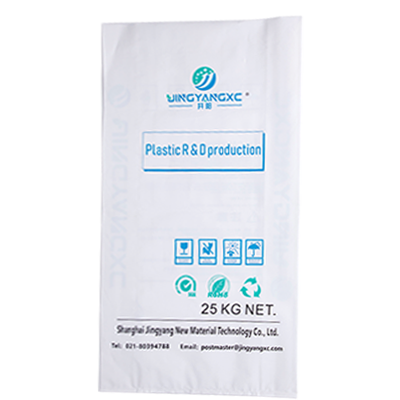
Reliability of aluminum-plastic heavy-duty bags is particularly critical for standard heavy packaging scenarios such as 25kg specifications. In chemical, construction material and food additive industries, a single damaged 25kg raw material package may cause thousands of yuan in product losses, transportation disputes and even damage to customer trust. Selecting high-performance aluminum-plastic heavy-duty bags is essential to mitigate risks at the source.
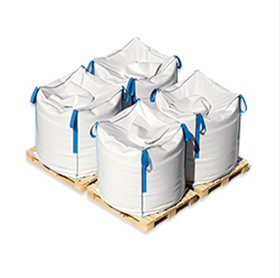
Star Group operates advanced production lines for aluminum-plastic film heavy-duty bags, specializing in aluminum-plastic composite FIBC bags and aluminum-plastic composite heavy-duty bags. Featuring light shielding to prevent photolysis, moisture and water resistance, airtight sealing against oxidation, and puncture resistance to avoid breakage, these products support load weights ranging from 20kg to 50kg. They are widely used for resin pellets, TPE synthetic rubber, biodegradable pellets, PBAT granules, lithium battery materials, metal powders and other materials.
Star Group boasts full in-house production capabilities covering cleanroom bag making, lamination and printing. Every production step undergoes strict quality inspection, including visual check, seal integrity, seal strength, pinhole and leakage test, pressure resistance, puncture resistance and bonding strength. Full-process quality supervision ensures stable and worry-free quality control.
With over 20 years of experience in custom industrial packaging, Star Group has solved packaging challenges for more than one hundred enterprises. Adhering to strict process standards, the group has obtained ISO9001, SGS, RoHS, REACH certifications and over one hundred patents. These qualifications are backed by a mature and rigorous manufacturing system.